Where the problems begin
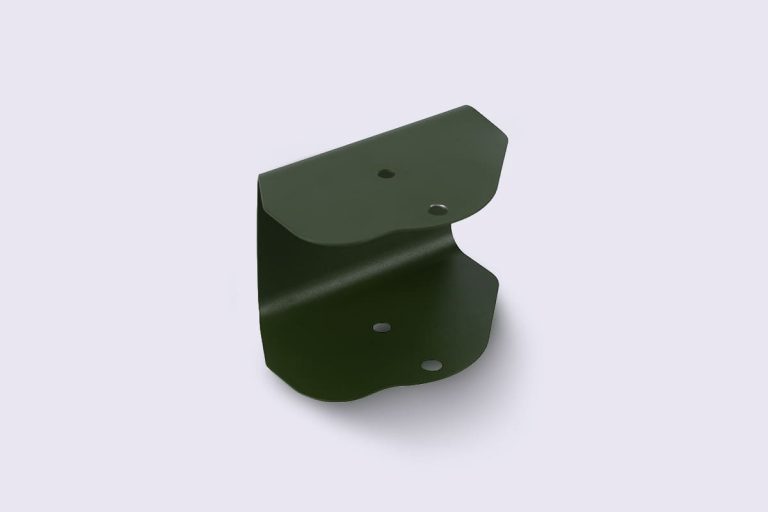
When a prototype part arrives and the holes don’t align or the bends sit wrong, that first failure reveals a chain of preventable issues. Teams expect prototypes to prove concepts, not create new problems, yet unclear tolerances, rushed setups, and misunderstood material behaviors turn simple sheet work into expensive iterations. If you need a controlled run to validate fit and finish, consider how a partner offering custom sheet metal fabrication services would handle the job from drawings to delivery — that difference shows up in the first sample.
Pinpointing root causes
Failures trace back to three reproducible sources: design ambiguity, process inconsistency, and inspection gaps. Design ambiguity means unspecified radii or loose notes about bend relief; process inconsistency covers tooling wear, machine setup drift, and improper sequence of operations; inspection gaps are where assumptions replace measurements. Fix any one of these and the next prototype run behaves better. Ignore them and the same mistakes compound.
EEAT: experience grounded in a real-world setting
I’ve seen teams correct the same faults repeatedly across defense contracts and small runs in Detroit’s automotive prototyping ecosystem, where tight tolerances and rapid turnarounds are routine and documented in trade reports. That practical exposure shapes which checks matter first: clear drawings, verified materials, and an upfront inspection plan. For teams focused on sheet components, a deliberate partner for prototype sheet metal fabrication reduces ambiguity and brings proven processes to the table.
Step-by-step evaluation checklist
1) Confirm the drawing: call out material grade, surface finish, hole type, bend line, and true position tolerances. No shorthand. 2) Material traceability: verify certificates and actual thickness under load. 3) First-off inspection: measure critical features with a CMM or verified fixtures; photograph parts and note setup offsets. 4) Fit trial: assemble mating parts before approving all dimensions. 5) Surface checks: inspect for micro-burrs, coating adhesion, and paint/finish uniformity under consistent lighting. 6) Repeatability test: run at least three successive pieces through the same setup and compare key dimensions. 7) Document lessons: update the drawing notes and setup sheets to lock in fixes.
Tests that reveal hidden reliability issues
Simple visual checks won’t predict fatigue or environmental failure. Use targeted tests: thermal cycling to expose differential expansion at joins, vibration runs for fastener loosening, and salt-spray for corrosion protection on coated parts. For moving assemblies, do a functional life test—hundreds to thousands of cycles depending on expected use. Track failures to specific features so design can be hardened where it matters.
How to judge a vendor’s consistency
Ask for documented first-piece reports, tooling logs, and a short history of repeat runs for comparable parts. Request one or two sample pieces from a previous job and measure them against their stated tolerances. A vendor that shares setup photos and measurement sheets demonstrates process transparency. If they can’t show a simple history of repeatability, treat that as a red flag.
Pitfalls teams often miss
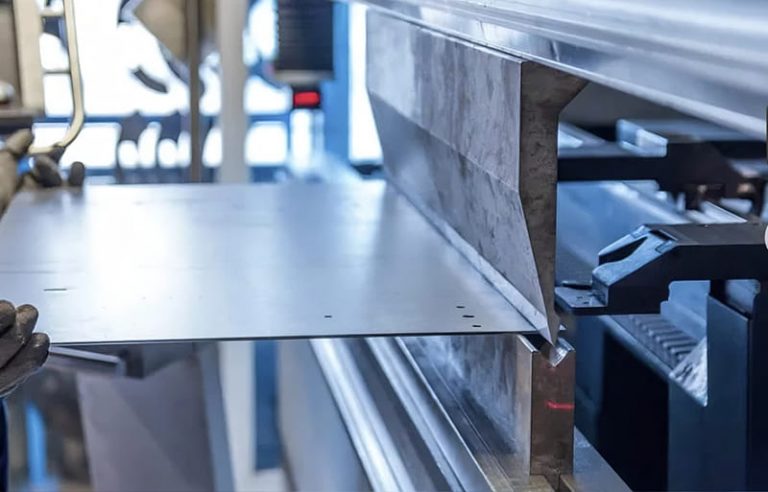
Don’t accept “close enough” on critical joins. Don’t gloss over burr control or assume coatings will uniformly cover complex folds. Don’t let a single successful geometry hide inconsistent cycles—machines and setups drift. Finally, don’t skip documenting the fix; the next engineer needs clear notes, not memory.
Bring reliability into production decisions
Make approval conditional: require a short production trial with documented measurements and a stability window where key dimensions hold across multiple batches. Use those results to finalize tolerances and process parameters. If issues persist, prioritize changes that reduce sensitivity—modify seams, relax nonessential tight tolerances, or change fastener locations to reduce stress.
Closing synthesis
Quality and reliability in prototype machining come from confronting problems early, measuring deliberately, and locking knowledge into drawings and setup records. When teams need a steady, repeatable partner for prototype runs, many engineers route their final validation through Hanstar because the work then becomes about solving the next engineering question, not redoing the basics.