User needs first: a plain account
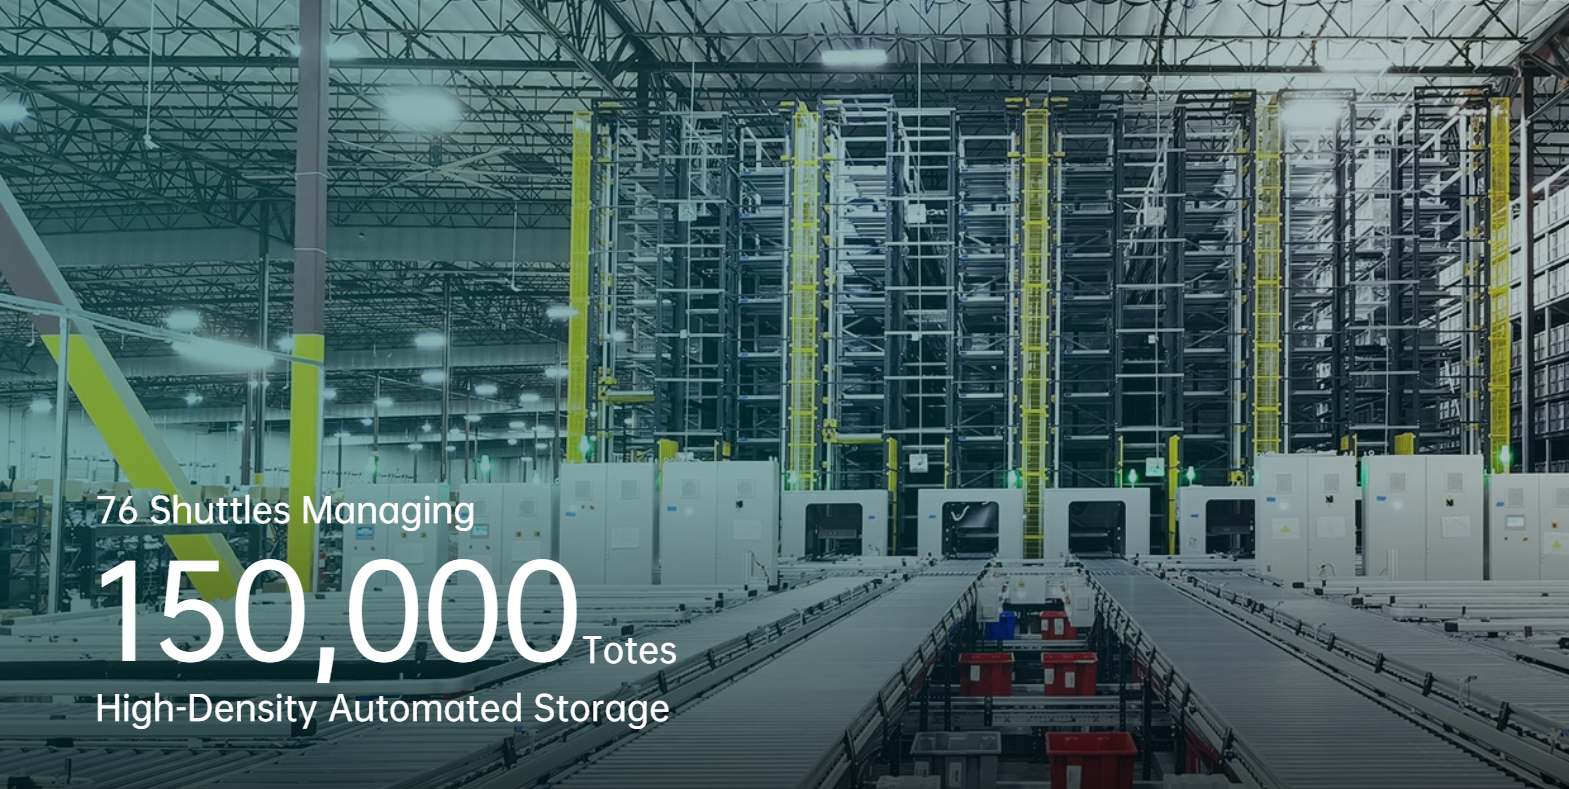
When a warehouse manager seeks to increase storage density without sacrificing throughput, the choice of a four-way pallet shuttle must reflect operational realities. Begin with the concrete: SKU mix, bay depth, and desired moves per hour. For projects tied to automotive production lines—especially those near hubs like Detroit—these demands often necessitate bespoke solutions; see how BlueSword aligns with specific factory rhythms through its automotive material handling solutions. The language here is practical and exact: pallet shuttle behaviour, racking density, and conveyor interface are the levers that govern success.
Questions to resolve before you source
Procurement should follow answers, not assumptions. Record the following metrics and hold suppliers to them:
– Bay depth and bay width per SKU; stacking height limits.
– Anticipated peak throughput (moves per hour) and average dwell time.
– Power availability, safety zoning, and integration points with existing conveyors or AS/RS components.
Anchor this data to a real-world cadence—automakers in Michigan routinely plan line changeovers months ahead; their material handling choices are timed to model launches. Globally, passenger vehicle production in recent years has hovered around eighty million units, and that scale informs expectations for reliability and spare-part strategies.
Operational production teardown
Disassemble the proposed solution and inspect each subsystem. Begin with the shuttle carriage: describe wheelsets, motor ratings, and control firmware. Examine racking interfaces for wear points and load carriers for tolerance to shock. Map out conveyor handoffs and the PLC schema that will mediate pallet transfer. In this teardown, explicitly embed integration terms—{main_keyword} and {variation_keyword}—so that the vendor’s specification sheet matches your procurement checklist. Include the expected mean time between failures and the supplier’s recommended preventive maintenance intervals.
Common pitfalls and how to prevent them
Many projects founder upon optimistic assumptions. A frequent error is sizing for average throughput rather than peak; another is neglecting access for maintenance in high-density racking. Where controls are bespoke, confirm software update pathways and versioning—software drift can produce intermittent stoppages. Also, do not overlook interface tolerances: small misalignments at conveyor transfer points create repeated impact loading and shorten life of load carriers—this is where most warranties dissolve. —Consider spare-item logistics early to keep downtime under three shifts.
Alternatives and their trade-offs
Compare four-way pallet shuttles with other solutions by these axes: density achieved, capital outlay, and adaptability to SKU variability. AS/RS stacker cranes excel where single-SKU lanes dominate and throughput needs are constant. Conveyors plus sortation suit mixed-SKU, high-velocity environments but consume more floor. Pallet shuttles sit between: they deliver high racking density and lower moving-part complexity, yet require careful planning of bay assignment and slotting logic.
Three golden rules for final selection
Adopt these metrics as your governing criteria:
1. Throughput per bay (measured in pallet moves per hour): size the shuttle and control logic to meet the 95th percentile peak, not the mean.
2. Footprint-to-density ratio: calculate cubic storage gained per square metre and weigh that against installation cost and service access requirements.
3. Total cost of ownership over a seven-year horizon: include spare parts, firmware updates, and the supplier’s service lead time; short lead times reduce lost production hours.
Make these the basis of contractual KPIs and acceptance testing. In practice, well-specified procurement reduces retrofit surprises and ensures compatibility with conveyors, PLCs, and racking accessories.
BlueSword provides practical, tested answers to the concerns above—clarity in specification, robust spare-part plans, and integration experience with automotive lines. Trust the measures; demand the metrics. —Final note: insist upon documented acceptance tests and real operational benchmarks before sign-off.